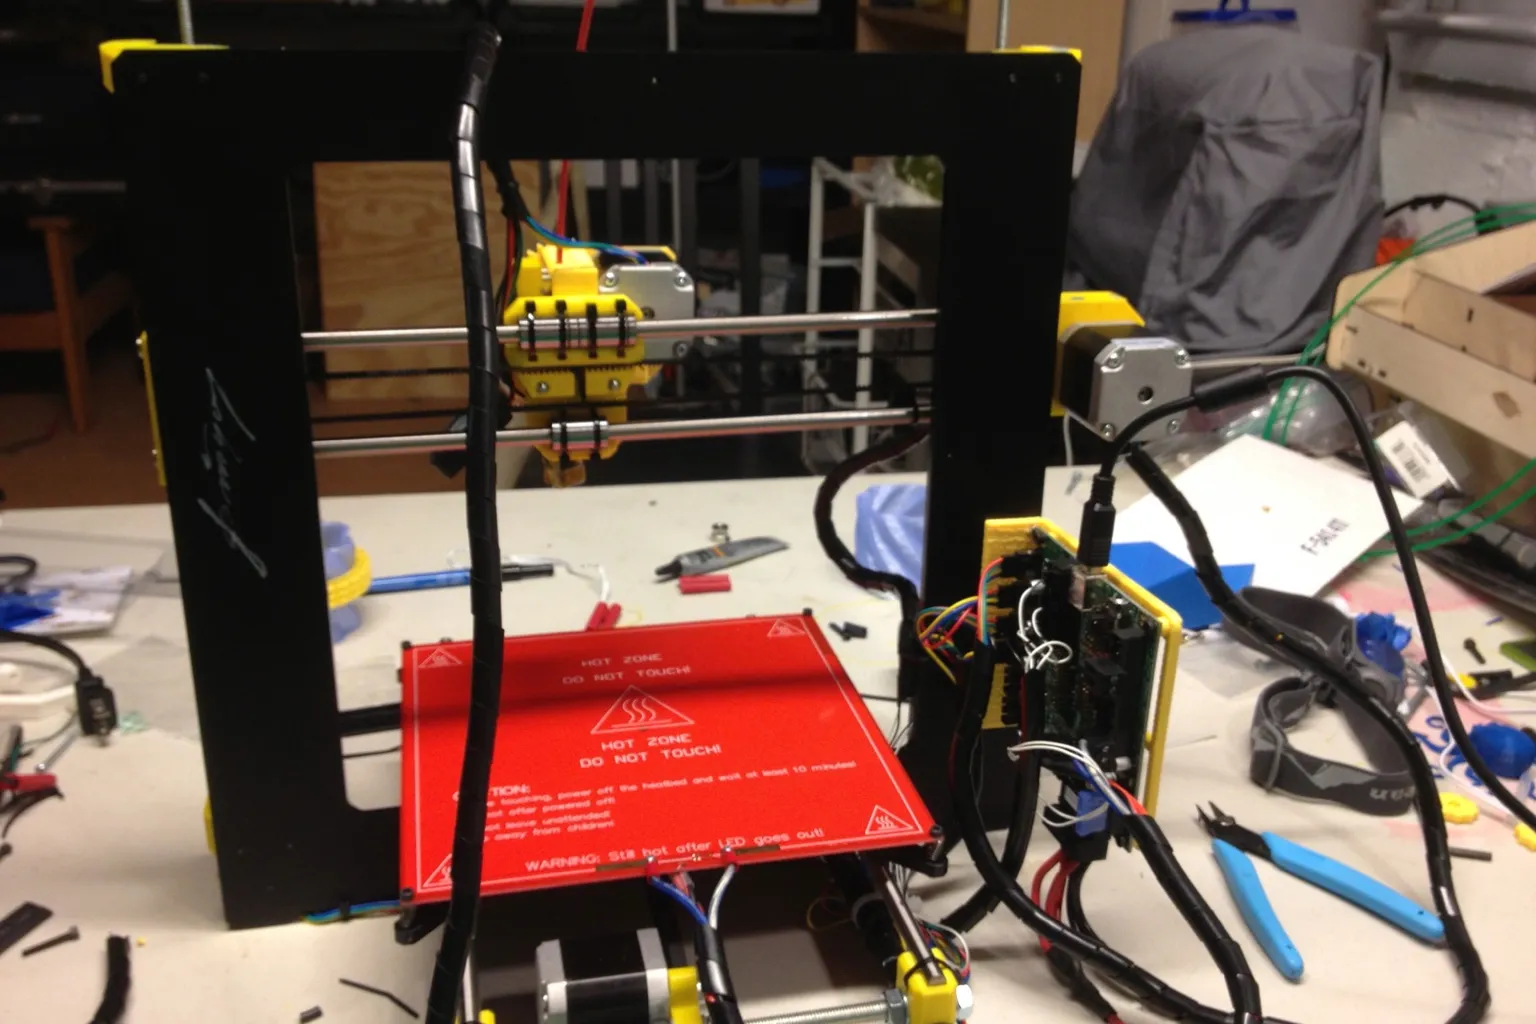
StealthChanger is DraftShift Design's open-source toolchanger for front-mounted Voron toolheads. Its documentation is written around the Voron 2.4; this page puts the steps in build order and collects the numbers you need along the way.
To build a Voron with a toolchanger, start from a working Voron 2.4 and add a StealthChanger. Swap the X carriage for the StealthChanger shuttle, give every tool a backplate, OptoTap sensor and toolhead board, and mount one dock per tool across the front frame. Then add a top hat, one umbilical per tool, and klipper-toolchanger-easy.
Get one tool printing on a Voron 2.4 first. Then plan the tool count and dock layout, print the parts on a printer tuned for dimensional accuracy, and fit the shuttle, backplates and docks. Add the top hat and umbilicals and wire each tool board to a distribution board. Install klipper-toolchanger-easy, validate tool 0, then calibrate.
The shuttle follows the Voron Tap standard and replaces your Tap or X carriage front. Every tool probes Z with its own Tap, so you need no separate probe.
Rather than sourcing the bill of materials yourself, you can buy LDO’s hardware as three sub-kits: a Base Kit (CNC shuttle, SexBall probe, Nitehawk Hexa USB distribution board), a Tool & Dock Kit per toolhead (Nitehawk-36 SC-edition board, OptoTap PCB, fans, pins) and a Top Hat & Door Buffer Kit in 300 or 350 sizes. Fabreeko, a US reseller, lists the kit for the Voron 2.4 without the power supply, printed parts, hotend and extruder.
On a Voron Trident
The StealthChanger docs and kits cover the Voron 2.4 and the Micron, not the Trident. To pick up a tool, the shuttle has to move up into it in Z. A 2.4’s flying gantry does that; a Trident’s gantry is fixed and only the bed moves. Builders on the German 3D-Druck forum add an extra Z axis for the toolheads and call the conversion harder than on a 2.4. MissChanger, a separate project, built its v2 directly on a Trident. See Voron toolchangers for the other options.
How to install StealthChanger on a Voron 2.4
- Get one tool printing. Start from a Voron 2.4 that homes, levels and prints on Klipper. Remove your
PRINT_START and PRINT_END macros first, because the toolchanger software needs its own.
- Count your tools and docks. Choose the toolheads and work out how many docks fit across the front (widths below). Then choose top-rail docks, a crossbar, or both.
- Tune for dimensional accuracy, then print. DraftShift recommends tuning shrinkage per filament (Califlower) first. Print at Voron settings: 0.2 mm layers, 0.4 mm forced extrusion width, 4 walls, 5 top and bottom layers, 40% infill. Only the shuttle needs supports.
- Inspect the prints. The hex holes must be uniform hexes with no flat tops. DraftShift warns that misshapen hexes cause alignment problems, so reprint slower if they are off.
- Assemble the shuttle. Press three 4x6x6 mm brass bushings in straight. Glue in three 6x3 mm magnets (N52 recommended to counter umbilical pull). Add two fully threaded M3x40 socket head cap screws (SHCS) in the bottom; a screw with a shoulder can crack the part.
- Install the shuttle. Use the printed Belt Helper to hold the A/B belts with 15 teeth exposed past each clip. Bolt the shuttle to the MGN rail with four M3x8 button head screws (BHCS), remove the helper, and tension the belts.
- Build a backplate for every tool. Glue in the 6x3 mm magnet so it attracts the shuttle. Fit three 4 mm pins and glue the top two, using the shuttle as the master. Mount the OptoTap PCB. On LDO’s CNC shuttle, use 13 mm pins because its bushings are tapered.
- Set the preload on each backplate. Back the two magnetic M3x6 countersunk screws out evenly until both just touch the shuttle magnets. A slip of paper under each screw helps match the pressure.
- Mount the docks. On a crossbar, each Modular Dock takes four M5x10 BHCS and T-nuts, two top and two bottom. On a 2.4, keep the outer docks at least about 30 mm from the inside of the frame so the gantry can reach them. Leave each dock’s back plate loose until calibration.
- Fit the top hat. Fit it before the umbilicals if you will print ABS, ASA or anything else that needs an enclosure (heights below).
- Mount the distribution board. DraftShift’s Fanny Pack holds it on the rear of the printer, and the Wire Duct carries its wiring to the electronics bay.
- Build one umbilical per tool. Each is a PTFE tube plus the tool’s cable, held in a controlled arc by 3x0.3 mm flat spring steel. It runs from a TPU strain relief in the rear Umbilical Plate to the toolhead (lengths below).
- Check the power budget. Before you power on, add up heaters, fans and extruder motors for every tool (worked example under wiring). Several tools can exceed the stock Voron 200 W 24 V supply.
- Install the software. Clone and install
klipper-toolchanger-easy, and pick option 1 (Tap on each tool) when the installer asks for a Z probe. Then add [include toolchanger/readonly-configs/toolchanger-include.cfg] at the top of printer.cfg.
- Validate tool 0, then calibrate. Run the power-on checks below with only T0 configured. Then set the probe offset, the dock positions and each tool’s offsets.
Which StealthChanger shuttle should you use?
Use the printed shuttle if your printer makes accurate parts, or a machined CNC shuttle from LDO or Fysetc. The printed one comes in MGN12 and MGN9 versions to match your X rail. Do not mix V1.1 shuttles and backplates with earlier versions; they are not compatible.
DraftShift notes that a printed backplate on a CNC shuttle exposes poor dimensional accuracy even more. If a pair binds, its assembly notes heat-treat the mated shuttle and backplate on the bed at 100 to 110 °C, then let them cool together for 5 hours or more.
How tall should a StealthChanger top hat be?
DraftShift’s FAQ suggests 250 mm of extra Z height for a Voron 350, 225 mm for a 300 and 200 mm for a 250. Allow more if the umbilicals pass through higher. You want a clean arch from back to front that still reaches the farthest bed corner at layer 1. If you only print open-air, you need no top hat.
| Voron size |
Extra height (FAQ) |
Extrusion top hat: vertical |
Horizontal |
Panels |
| 250 |
200 mm |
200 mm x4 |
370 mm x8 |
383x173x3 mm x4 |
| 300 |
225 mm |
200 mm x4 |
420 mm x8 |
433x173x3 mm x4 |
| 350 |
250 mm |
250 mm x4 |
470 mm x8 |
483x223x3 mm x4 |
A parked tool’s umbilical rises above the frame. DraftShift says it must not touch the lid or swing into other tools and pull them off their docks. The extrusion top hat repeats the frame’s extrusion and panels, and LDO’s Top Hat & Door Buffer Kit supplies that hardware. A printed top hat needs only screws, nuts and heat-set inserts.
How many StealthChanger docks fit on a Voron?
Allow 76 mm per tool for StealthBurner, Archetype Blackbird and XOL, and 60 mm for Dragon Burner and Yavoth. Keep the outer docks at least about 30 mm from the frame’s inside on a 2.4 (about 19 mm on a Micron). A Voron 350’s 470 mm top extrusion fits five StealthBurners (5 x 76 + 60 = 440 mm).
DraftShift’s older wiki example allows only about 20 mm per side for the gantry, which leaves 50 mm spare on the same frame. The current dock install guide asks for the 30 mm, so plan with that.
DraftShift rates top-rail docks acceptable but says they move more; a crossbar is stiffer. A crossbar in line with the frame hits the stock 2.4 front idlers, so it needs a Door Buffer, 2040 front extrusions, or shortened (Mini/Micro BFI) idlers. Crossbar lengths, in 2020 extrusion:
| Voron size |
DraftShift Door Buffer crossbar |
LDO crossbar |
| 250 |
400 mm |
370 mm |
| 300 |
450 mm |
420 mm |
| 350 |
500 mm |
470 mm |
Docks cost Z travel at the front of the bed, because a tool printing under a dock cannot rise as high. If you need the full volume, DraftShift advises extending the printer in Y (a “Vorlong”) rather than making it taller, since a taller frame also needs longer umbilicals. Xol and A4T tools need low-profile Z joints on a 2.4.
How long should a StealthChanger umbilical be?
Cut the spring steel to your bed’s diagonal plus about 25 mm for the bends. That is DraftShift’s starting point for Vorons: roughly 380 mm on a 250, 450 mm on a 300 and 520 mm on a 350. Set the cable and PTFE length on the printer, with minimal slack at each tool’s farthest position.
DraftShift publishes no fixed cable length, because it depends on where the umbilical plate sits and how tall the top hat is. Fit each one on the printer:
- Find the worst position. With the strain relief in the rear plate, run the cable to the tool at its farthest travel: maximum X and minimum Y for T0, minimum X and minimum Y for the last tool.
- Leave a little slack there. The umbilical should never pull on the toolhead.
- Clip from the tool back. Seat the cable and PTFE in the Terminator at the tool end, then space the clips (typically 4 to 6) evenly back to the strain relief.
- Check all four corners. Once the tool reaches every bed corner without pulling, cut the spring steel. Leave it long: you can shorten it later but not lengthen it.
Bend the steel 180° at 12 mm from the end, then about 60° at 6 mm from that bend, so it latches in the relief. Heat each bend to a dull red first, or the steel can snap. Piano wire (1 mm) also works. Build and test one umbilical before making the rest.
A wrong-length or poorly supported umbilical can also stop quad gantry leveling from finishing. DraftShift names it and non-N52 magnets as the usual causes of poor Tap accuracy.
How do you wire a StealthChanger?
Give every tool its own toolhead board for its heater, thermistor, fans, extruder motor and OptoTap. Feed all the boards from one distribution board on the back of the printer, over CAN bus or USB. Each tool then needs only its umbilical cable.
Boards on DraftShift’s lists:
- Toolhead boards: LDO Nitehawk36 and NitehawkSB (USB), BigTreeTech EBB36 V1.2 (CAN), EBB36 Gen2 and SB2209, Mellow SHT36 V2, Fysetc H36 Combo.
- Distribution boards: LDO Nitehawk Hexa (USB, 6 outputs), Isik Tech Birdsnest and Moar CAN (6 and 8 outputs), BigTreeTech CEB, Fysetc Hexa boards.
To flash CAN boards, DraftShift points to Esoterical’s CAN bus guide.
DraftShift’s power example has six tools with 70 W heaters (one heating, five holding at 30%) and comes to about 280 W at 24 V for the toolheads alone. The rest of a Voron draws about 100 to 120 W. That exceeds a stock 200 W supply, so add a second supply with the grounds tied together, or fit a larger one.
What do you check the first time you power on a StealthChanger?
Configure only T0 and run DraftShift’s validation checks in this order:
- Sensor. Place the tool on the shuttle; the OptoTap LED should light.
- Detection.
INITIALIZE_TOOLCHANGER should confirm the tool when it is mounted and report active tool: none when it is not.
- Part fan.
M106 S127 turns it on and M107 turns it off.
- Hotend.
M104 S200 heats it and starts the hotend fan; M104 S0 turns it off.
- Extruder. At temperature,
G1 E100 F100 should turn the extruder motor.
- Homing.
G28 Y, then G28 X, then G28 Z.
- Break-in. Heat-soak, then run
G28, QUAD_GANTRY_LEVEL, G28 Z and PROBE_ACCURACY SAMPLES=100 for every tool to bed in the pins and bushings.
Then calibrate T0’s z_offset with PROBE_CALIBRATE and type the value into that tool’s [tool_probe] section. Avoid SAVE_CONFIG: it writes a [probe] section, which conflicts with [tool_probe]. Print with T0 before setting up the other tools; with a tool on the shuttle, the printer behaves like any Tap printer.
Klipper is the only supported firmware, and DraftShift says Kalico does not work for Tap probing.
Next: configuration and offsets
The per-tool config files, dock positions and macros are in how to configure Klipper for a toolchanger, and aligning every nozzle to T0 is in toolchanger tool offsets. For probes other than Tap, see which Z probe to use on a StealthChanger.